
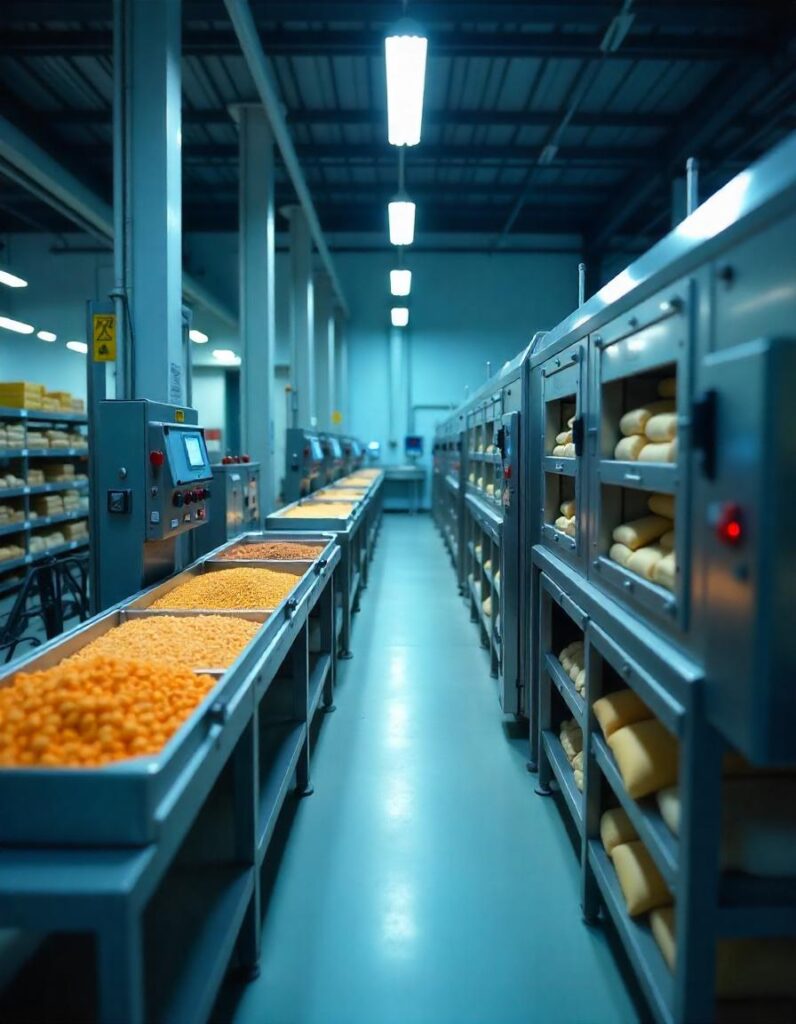
Case Study – Food Production Plant
A leading food manufacturer managing a large number of fixed assets across diverse areas of its plant: production, warehouse and office.
Read more

Examples of RFID implementations in manufacturing, retail and logistics. We show how a well-designed RFID system streamlines processes, reduces operational errors, delivers measurable financial benefits and improves the security of business operations.
A leading food manufacturer managing a large number of fixed assets across diverse areas of its plant: production, warehouse and office.
Read more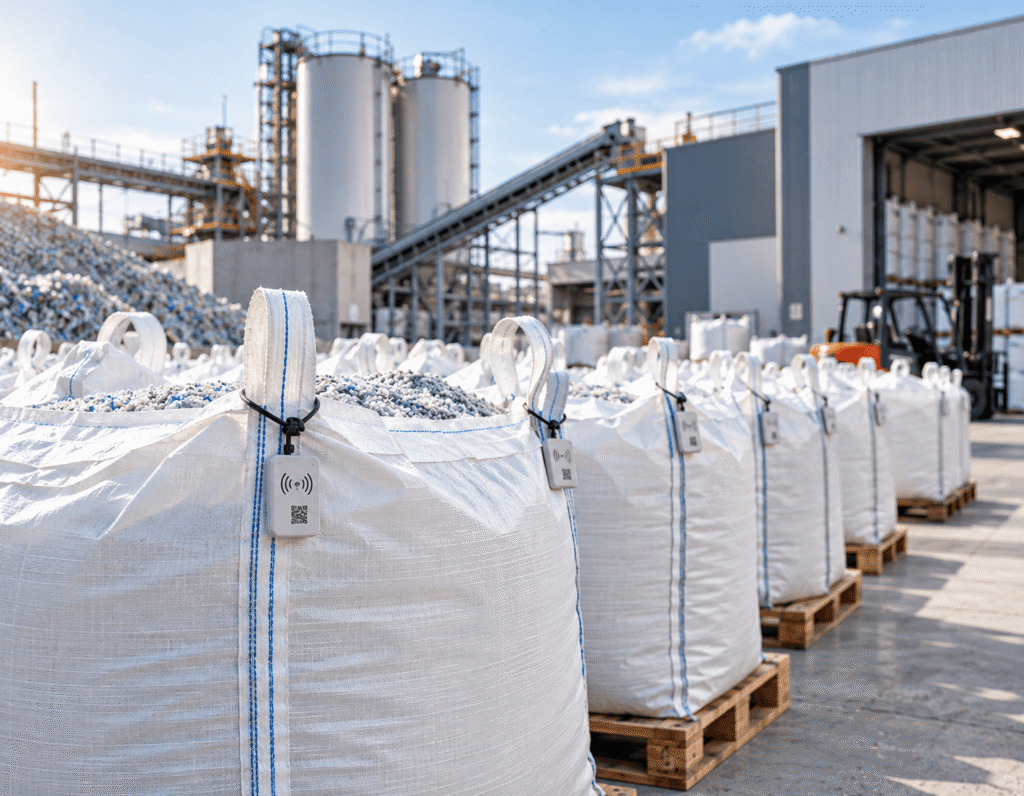
A UHF RFID system that automatically tracks the flow of big bags between logistics, production, quality control and the warehouse.
Read more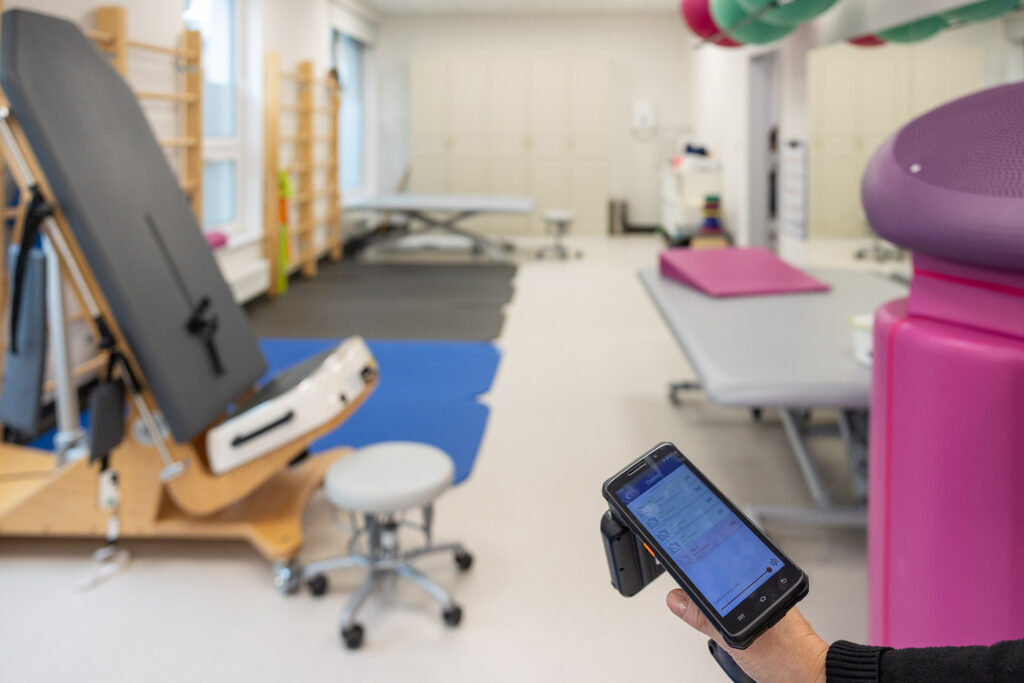
See how an RFID system can help staff locate and manage therapy equipment at a rehabilitation centre.
Read more
Learn how automated RFID inventory helps service teams check equipment in their vehicles and keep track of essential tools.
Read more
Find out how RFID helps a shooting club identify and control firearms and equipment, supporting accurate inventory and oversight.
Read more
Discover how RFID enables self-service sales and automatic product counting at a flower wholesaler’s checkout.
Read more